What is Food-Safe Flooring?
In the food and beverage industry, safety begins from the ground up. Food-safe flooring refers to specialised surface solutions engineered to meet rigid sanitary standards, preventing contamination, resisting bacterial growth, and enduring harsh processing conditions.
Unlike standard commercial surfaces, a true food-grade flooring system must be entirely non-porous, monolithic (seamless), and free of cracks, joints, or grout lines where organic matter, moisture, and pathogens can accumulate.
Unprotected concrete substrates are inherently porous, acting like a sponge for liquids, proteins, and biochemical waste. When left exposed, they become hotbeds for dangerous microbes such as Listeria, Salmonella, and E. coli.
Implementing specialised surfaces eliminates these micro-vulnerabilities, creating an easily sanitizable envelope that stands up to aggressive thermal and mechanical stress.
Facilities Requiring Specialised Sanitary Flooring
Compliance and hygienic protection are vital across various operational sectors. Any environment involved in processing, packaging, or serving food requires rigorous surface controls:
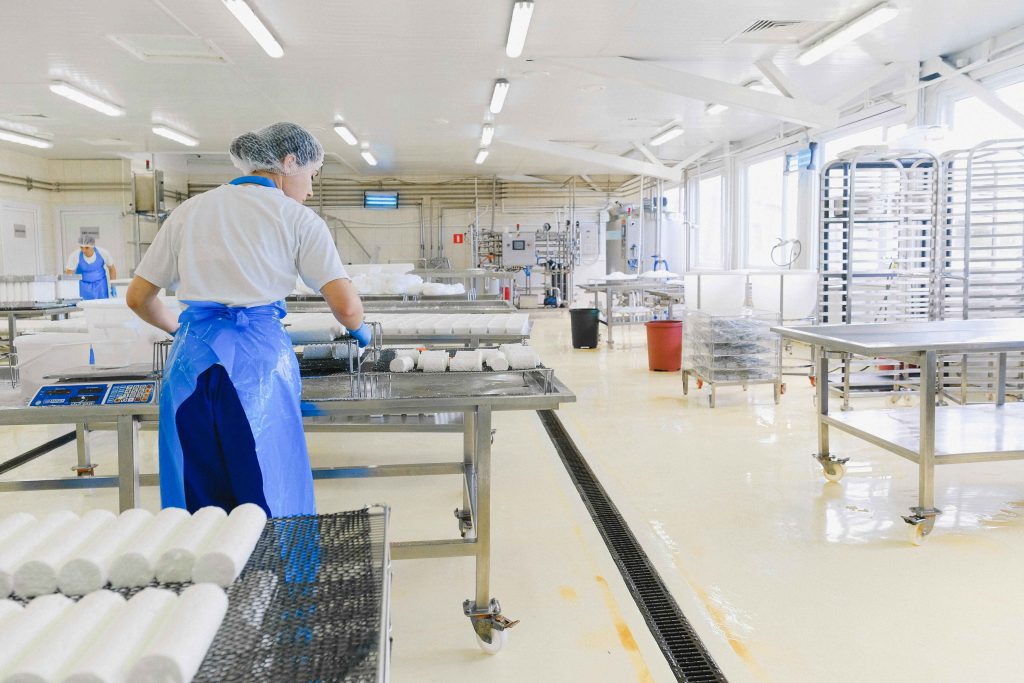
- Food Processing Plants: Meat, poultry, seafood, and dairy processing facilities dealing with heavy organic residue and intense moisture.
- Industrial Bakeries & Confectioneries: Environments constantly subjected to high ambient heat, dry ingredient powders, sugar residues, and intensive baking fats.
- Beverage and Bottling Facilities: Operations characterised by high-volume fluid transit, acidic fruit juices, chemical clean-in-place (CIP) washdowns, and thermal shock.
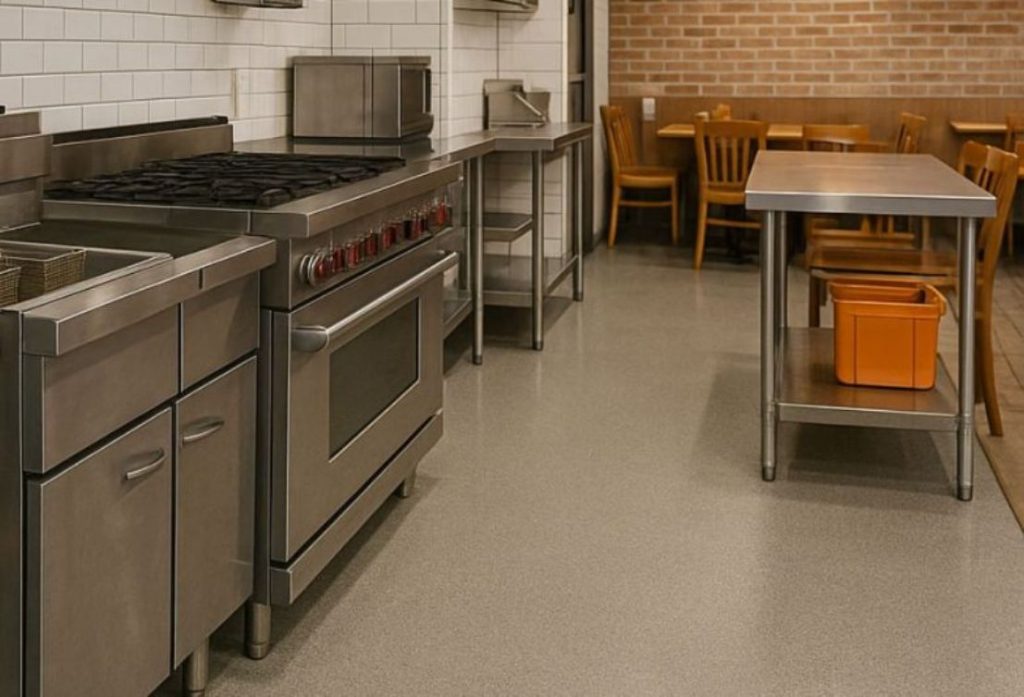
- Commercial Kitchens & Food Preparation Areas: Heavy foot traffic, frequent spillages of boiling oils, and rapid turnarounds require specialised commercial kitchen epoxy flooring.
- Dining and Public Front-of-House: High-traffic spaces requiring attractive, wear-resistant, and easily cleanable surfaces like restaurant epoxy flooring to ensure public health safety.
- Cold Storage Facilities & Freezers: Sub-zero storage spaces that require materials resilient against severe thermal contraction and continuous low temperatures.
Why Food-Safe Flooring is Important
Food-safe flooring systems are crucial for a number of reasons related to regulatory compliance, safety, and hygiene.
Hygiene Compliance (HACCP & GMP Standards)
Regulatory compliance is a critical requirement in modern food manufacturing. Facilities must fulfil international standards such as Hazard Analysis Critical Control Point (HACCP) and Good Manufacturing Practices (GMP). Choosing certified food-safe resin flooring ensures that your floors cease to be a “critical control point” for biological contamination. HACCP certification guarantees that the flooring material has been strictly evaluated for chemical emissions, non-toxicity, ease of sanitisation, and structural integrity under industrial loads.
Slip Resistance for Operational Safety
Food processing areas are routinely compromised by wet or oily substances, creating severe slip-and-fall hazards. To secure workplace safety, industrial floors are rated on a German slip resistance scale from R9 (lowest slip resistance) to R13 (highest slip resistance). Food environments typically demand a rating between R9 and R12.
Chemical Contact Resistance
Industrial floors face frequent exposure to highly corrosive substances, including organic acids (oleic, citric, and lactic acids from dairy, blood, and citrus juices) and inorganic chemicals used during sanitation. Without robust food-safe industrial flooring, these chemicals erode the matrix of standard concrete, generating dust and potholes that harbour dangerous bacteria.
Rigorous Cleaning and Maintenance
Sanitation protocols require heavy-duty pressure washing, steam cleaning, and aggressive alkaline or acidic detergents. Food-safe surfaces must endure these cleaning routines day after day without blistering, peeling, or degrading, preserving a perfectly seamless barrier over the life of the building.
Durability and Longevity
Beyond chemical and biological threats, floors endure gruelling mechanical stress from heavy forklifts, pallet jacks, and heavy stainless steel machinery. True industrial-grade systems resist impact damage, cracking, and abrasion, ensuring long-term structural integrity and minimising costly operational shutdowns for floor repairs.
| Stress Factor | Standard Concrete Performance | Food-Grade Polyurethane/Epoxy Performance |
| Lactic & Organic Acids | Rapid erosion, pitting, and dust creation | Excellent chemical resistance; no surface breakdown |
| Steam Cleaning / Hot Water | Thermal cracking and structural fracturing | High thermal shock threshold (withstands up to 120°C) |
| Bacterial Colonization | High risk inside porous cavities and grout | Zero penetration; seamless antimicrobial profile |
| Heavy Wheel Impact | Chipping, spalling, and crack propagation | High compressive and tensile strength; resists impact |
Best Food-Safe Resin Flooring Solutions
When specifying surfaces for high-compliance zones, resinous materials outperform all other alternatives. The two leading technologies implemented globally are epoxy flooring systems and polyurethane (PU) concrete systems.
Food-Safe Epoxy Flooring
As a foundational solution for dry processing zones, packing rooms, and commercial service spaces, food-safe epoxy flooring provides a rigid, highly aesthetic, and chemically resistant barrier. Epoxy systems bond tightly to concrete substrates, providing incredible compressive strength and an exceptionally smooth or textured finish. They excel in front-of-house restaurant spaces, laboratories, and dry storage facilities where rapid sanitisation and clean aesthetics are required.
Polyurethane (PU) Concrete Flooring System
For heavy-duty, wet-process environments, Polyurethane (PU) concrete systems represent the benchmark of modern engineering. PU systems are uniquely resilient against thermal shock, meaning they can withstand instantaneous temperature swings from boiling water washdowns or sub-zero blast freezers without delaminating from the concrete. Additionally, polyurethane concrete exhibits a thermal expansion coefficient similar to the concrete beneath it, moving in tandem with the building and eliminating stress-cracking.
Food-Safe Flooring Systems at Floorfinder
Floorfinder engineers a comprehensive suite of highly specialised resin flooring products tailored explicitly for the rigorous demands of the global food industry.
FLOORFINDER UNIVERSAL
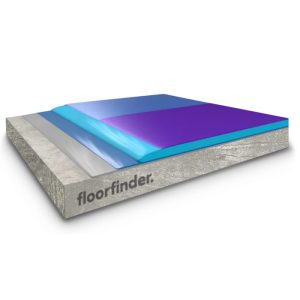
FLOORFINDER UNIVERSAL is a high-performance, solvent-free epoxy coating system engineered for outstanding wear resistance and easy cleaning. This versatile system is ideal for food-safe manufacturing facilities, dry packaging zones, and corridors where chemical exposures are common. It features high abrasion resistance, superior chemical shielding, and can be customised with optional slip resistance profiles ranging from R9, R10, to R11 to balance grip and ease of washdowns.
FLOORFINDER UNIFLEX
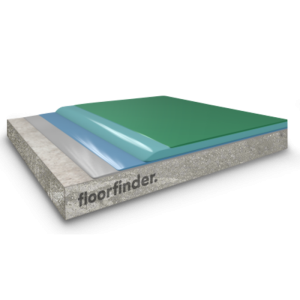
Designed for food processing and preparation areas requiring hygienic performance, durability, and design flexibility, FLOORFINDER UNIFLEX is a versatile polyurethane resin-based coating system engineered for light to medium mechanical and chemical loads. Its statically crack-bridging properties help protect against minor substrate movement, while the seamless, liquid-tight surface creates a hygienic barrier that is easy to maintain. With low emissions compliant with AgBB and other standards, excellent UV and colour stability, and slip-resistant surface options (R9–R11), this system provides a safe and reliable flooring solution for demanding food environments.
FLOORCRETE MF Standard
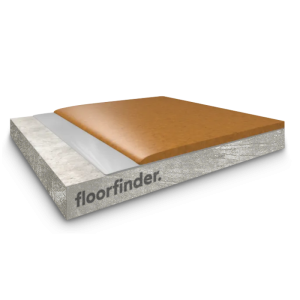
For demanding food-processing environments, the FLOORCRETE MF Standard provides heavy-duty defence. This self-levelling polyurethane concrete system is officially HACCP International certified, ensuring complete peace of mind for rigorous food audits. Formulated with ultra-low VOC emissions, it provides an R9 slip resistance profile, excellent resistance to aggressive industrial chemicals, and exceptional thermal shock resistance against severe temperature fluctuations.
Food-Grade Flooring Projects Using FLOORFINDER
Floorfinder systems have a proven track record of solving real-world structural and sanitation challenges in major food processing facilities across Asia.
Coffee Manufacturing Plant in Thailand
System Deployed: FLOORFINDER UNIVERSAL
A major coffee production facility faced hygiene compliance risks because its porous, untreated concrete floor absorbed moisture and corrosive, fermenting sugar residues. To solve this,
Floorfinder upgraded the production floor with the FLOORFINDER UNIVERSAL epoxy system. This seamless, dense resin barrier eliminated substrate vulnerabilities, providing superior abrasion resistance against heavy traffic, preventing sugar bonding, and enabling rapid washdowns to meet strict food safety regulations.
Francestle Confectioneries
System Deployed: FLOORCRETE PU-MF
Francestle Confectioneries‘ chocolate manufacturing facility faced severe risks of floor blistering and delamination due to inconsistent moisture levels in its concrete substrate, which threatened its strict hygiene compliance.
Floorfinder resolved this by engineering a multi-layered solution, applying a specialised solvent-free epoxy primer as a moisture barrier, followed by the heavy-duty FLOORCRETE PU-MF polyurethane concrete system. The resulting seamless finish provides long-term structural durability and uncompromised hygiene, easily withstanding the facility’s unique wet-cleaning cycles and temperature shifts.
Conclusion
Selecting the correct surface solution is an investment in your facility’s safety, compliance, and long-term operational efficiency. Floorfinder delivers precisely engineered systems tailored to your environment. As a trusted PU flooring manufacturer and epoxy floor specialist, Floorfinder provides the technical expertise and high-performance materials your facility demands. Contact Floorfinder today for tailored, HACCP-certified resin flooring systems.